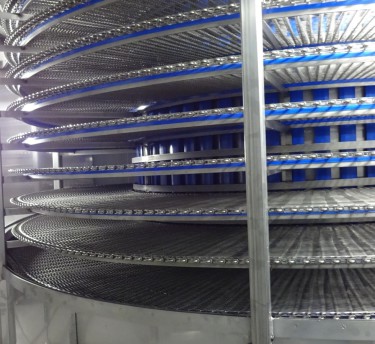
Re-configuring an Existing Spiral Freezer for Greater Production Flexibility
The situation
When production requirements change, replacing an entire system is not always the most practical solution.
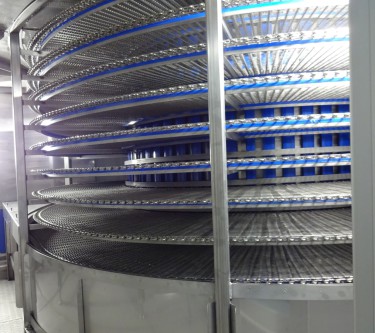
For this ice cream manufacturing project, Lomax were asked to upgrade and modify an existing twin drum spiral freezer serving an established ice cream production line. The aim was to adapt the existing equipment to better meet changing production requirements and accommodate different product formats.
The system needed to handle 900 ml tubs at 90 ppm and 1300 ml tubs at 75 ppm, while providing the flexibility required for the customer's production operation.
Rather than replacing the complete freezer, the project focused on understanding the existing system and identifying how its configuration could be re-engineered to deliver the required performance.
The challenge
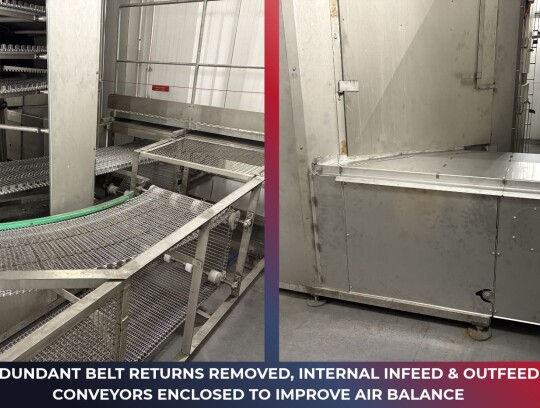
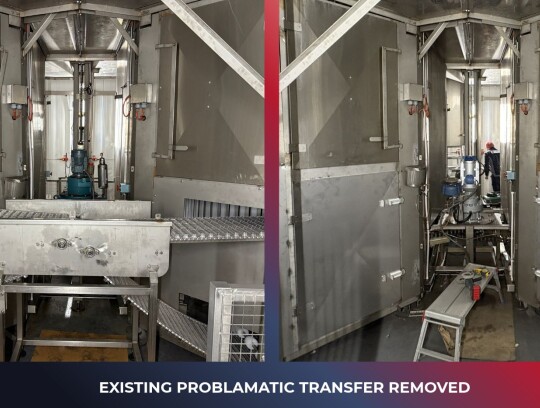
The freezer was originally installed as a twin-belt system with x2 infeeds and x2 outfeeds. At some stage it was modified by others, retaining the twin-belt configuration but reducing to x1 infeed and x1 outfeed (essentially product now travelled around the system twice before exiting), this introduced a problematic transfer between the drums where the product transitions from belt 1 to belt 2.
The challenge was to modify the existing system while maintaining the core structure and creating a new configuration capable of achieving the required belt pitch, tier spacing and retention time for the client to achieve their revised product formats and production rates.
This required careful consideration of how the two drums would work together once the system was converted to a single continuous belt.
The solution also needed to incorporate 20 tiers per drum, as specified in the customer's requirements, while removing the existing belt support arms from the main columns and resetting the tier spacing across both drums.
engineering the right solution
Lomax approached the project by working from the required production output back through the mechanical configuration of the freezer.The key requirement was to create a configuration that could accommodate the different tub formats and production rates while maintaining the required belt arrangement through the spiral system and remove the problematic transfer between drums.
This meant reassessing the relationship between the two drums, belt pitch and tier spacing rather than simply modifying individual components.
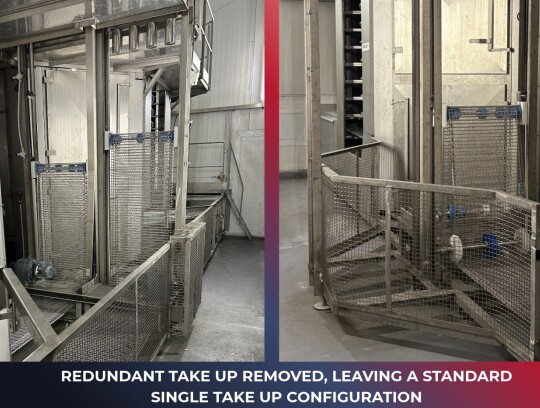
The existing system was reconfigured around a single continuous belt, with the transfer between the drums removed. Tier spacing was reset across both drums to achieve the required arrangement for the revised production requirements.
design decisions that mattered
One of the most important decisions was converting the system from a dual-belt configuration to a single continuous belt. This simplified the overall belt arrangement and provided the basis for the revised product flow.
The second key decision was to modify the tier pitch spacing across both drums. With 20 tiers required per drum, achieving the correct spacing was essential to creating the required belt pitch and spiral configuration.
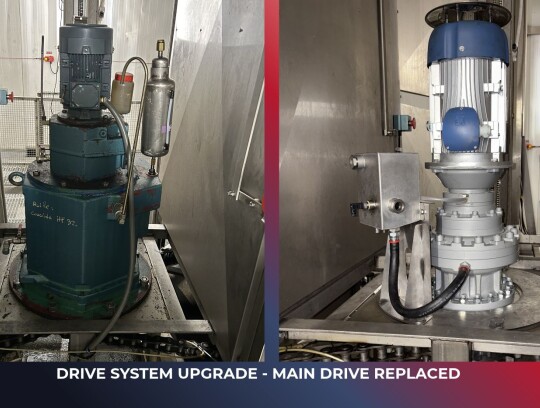
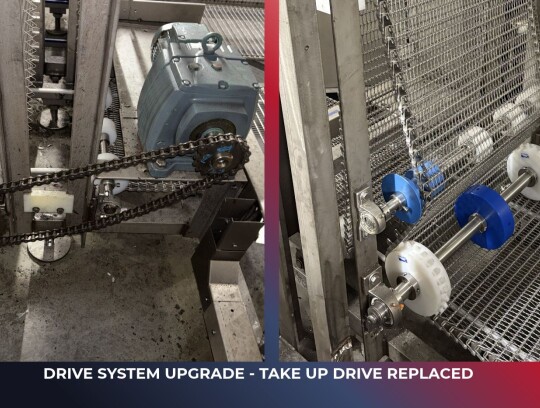
To achieve the required belt speeds and product loadings an upgraded drive system was also selected offering a wider retention time range along with higher output torque to handle the increased production volume.
the solution
The completed solution was an upgraded and reconfigured twin drum spiral freezer incorporating a single continuous belt, revised tier spacing and the required belt pitch and spiral arrangement.
The existing equipment was adapted rather than completely replaced, providing a practical route to meet the customer's updated production requirements while retaining the core freezer system.
delivery and commissioning
Lomax managed the project through the key stages of engineering, detailed design, manufacture, shipping, installation, commissioning and handover.
YOU MAY ALSO LIKE
New Single Drum Spiral for Leading UK Bakery
Go Big or Go Home
Lomax complete installation of two Spiral Freezer Hardening Tunnels for a leading ice cream producer in the USA.
Lomax Deliver Thailand Project
Spiral Freezer Relocation